In applications such as urban water supply, water conservancy and agricultural irrigation, industrial circulating water systems, and large scale pumping stations, whenever there is a demand for high flow and high head water transfer, a horizontal split case centrifugal pump is often one of the preferred solutions. Although it is also a type of centrifugal pump, a conventional pump may struggle to handle large flow requirements, while an axially split centrifugal pump can efficiently transfer large volumes of water. So, what enables it to achieve such high flow rates, and how does it work internally?
This article explains the working principle of a centrifugal split case pump in simple and easy to understand language. Whether you are new to the pump industry or involved in pump purchasing and selection, you can quickly understand how this type of pump works and why it is suitable for large flow applications.
1. What Is a Split Case Pump?
A centrifugal split case pump is also known as a single stage, double suction centrifugal pump. Its most distinctive feature is that the pump casing is horizontally split along the centerline. This design makes installation, disassembly, maintenance, and inspection more convenient, as the main components can be accessed without removing the connected pipelines or motor.
The key difference between a split case pump and a single suction pump is the double suction impeller. This is also one of the main reasons why a horizontal split case centrifugal pump can achieve a high flow rate.
As a type of axially split centrifugal pump, its horizontally split casing also provides convenient access to the internal components, making it well suited for applications requiring regular maintenance or long term continuous operation.
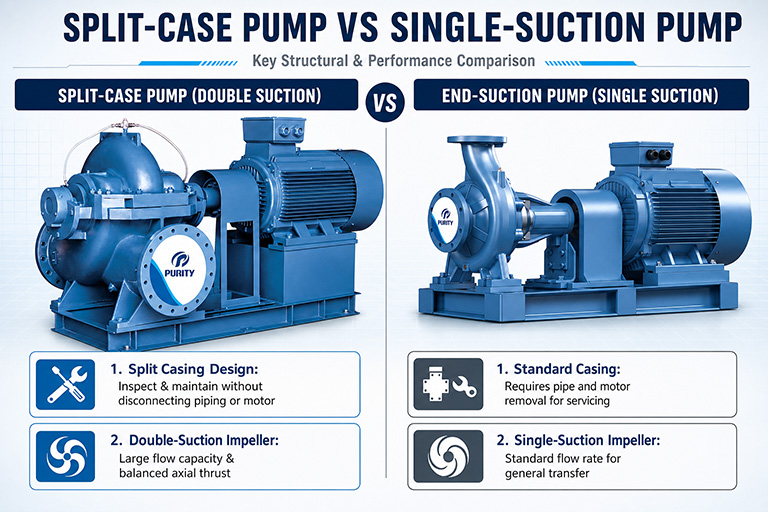
Picture|Purity Double Suction Split Case Pump vs Single Suction Pump
2. How Does a Split Case Pump Achieve High Flow?
A conventional single suction pump has only one water inlet, so water enters the impeller from one side. In contrast, a split case pump uses a symmetrical double suction impeller with an inlet on each side. Water enters the impeller from both sides simultaneously.
With the same rotational speed and similar impeller dimensions, the double suction design provides a larger effective inlet area and allows more water to enter the impeller within the same period of time. As a result, the pump can achieve a much higher flow rate than many conventional single suction pumps.
The symmetrical hydraulic passages also help reduce hydraulic losses and improve operating efficiency. Depending on the specific design and operating conditions, pump efficiency can typically reach around 85%–94%. Compared with conventional single suction pumps, this can provide significant energy saving benefits, especially when the pump operates continuously at high power.
This is why axially split centrifugal pumps are widely used where high flow, stable operation, and reliable long term performance are required.
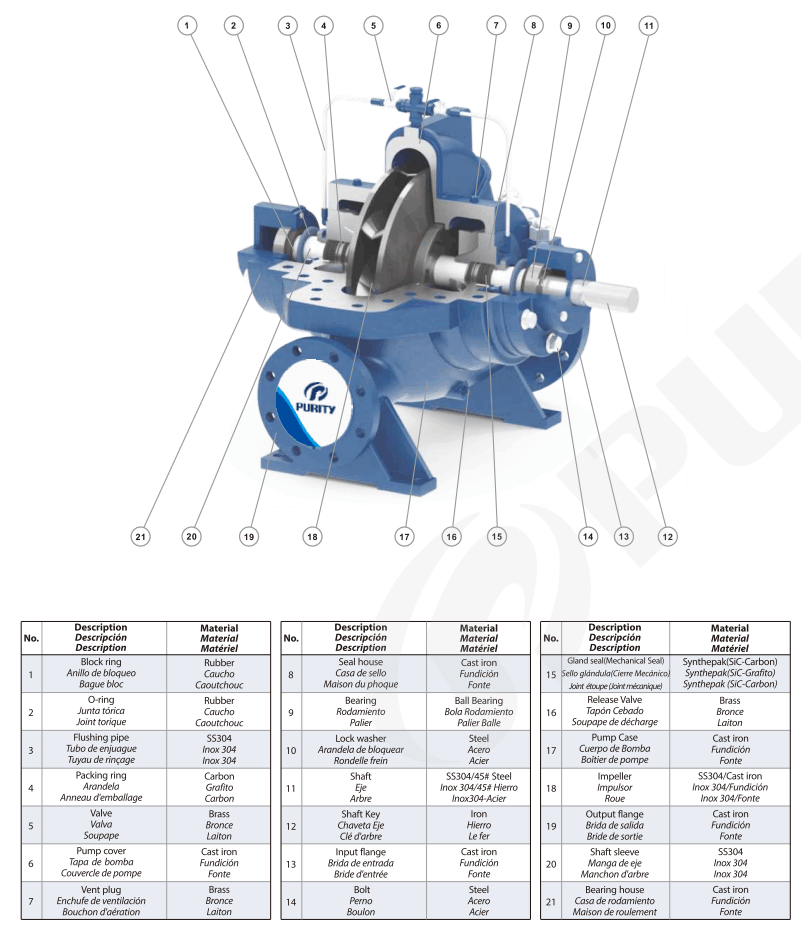
Picture|Centrifugal Pump Components
3. Where Are Split Case Pumps Used?
With their advantages of high flow, high efficiency, stable operation, and convenient maintenance, split case pumps are widely used in many applications, including:
·Urban water supply and municipal drainage systems
·Agricultural irrigation, reservoir water transfer, flood control, and drainage
·Industrial circulating cooling water and large flow chemical fluid transfer
·Central air conditioning water circulation systems
·Large scale pumping stations and water transfer projects
For fire protection applications, a specially configured electric split case fire pump can also be used to provide reliable high flow water supply for fire fighting systems.
4. Why Choose the Purity PSCM Split Case Centrifugal Pump?
Reliable Structural Design:The Purity PSCM adopts an axially split volute casing design. Its stable construction makes disassembly, maintenance, and inspection more convenient, making it suitable for long term continuous operation.
Durable Pump Casing:The pump casing is made of corrosion resistant HT250 cast iron, offering good mechanical strength and durability for a variety of operating conditions.
High Quality Impeller Options:The impeller can be made of AISI 304 or HT250, combining corrosion resistance and mechanical strength to meet the requirements of different pumping media and applications.
Effective Shaft Protection:The pump shaft is protected by a corrosion resistant shaft sleeve, which helps reduce corrosion and wear while extending the service life of the shaft.
Flexible Sealing Options:The pump supports both mechanical seals and packing seals, allowing the sealing method to be selected according to different operating conditions and customer requirements.
High Strength Bearings:High strength rolling bearings provide stable and reliable operation, helping reduce wear and extend the service life of the equipment.
Flexible Power Options:The pump can be equipped with either an electric motor or a diesel engine according to actual application requirements. This makes it suitable for water supply, fire protection, and other applications where stable and reliable operation is essential.
As a centrifugal split case pump, the PSCM combines high flow hydraulic performance with a practical split casing structure, making it a reliable choice for demanding water transfer applications.
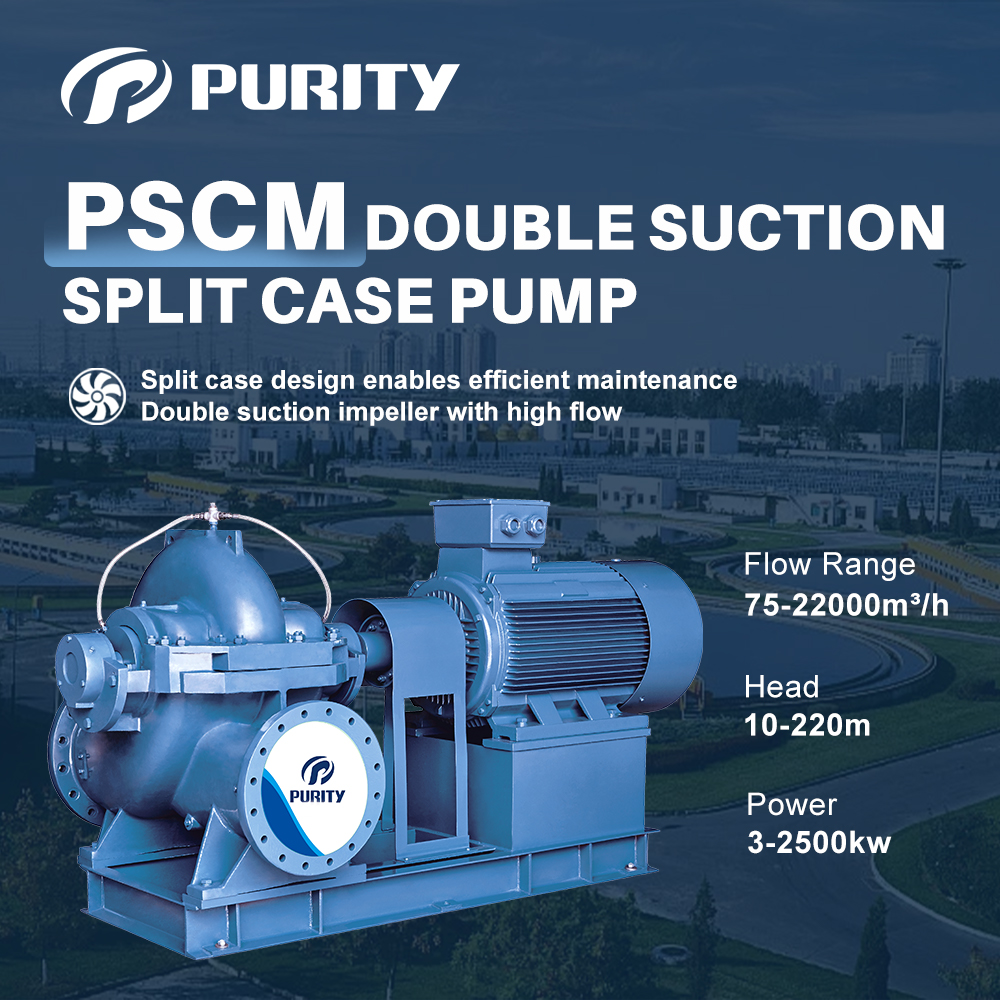
Picture|Purity PSCM Split Case Centrifugal Pump
5. Conclusion
The reason split case pumps have become a major solution for high flow water transfer lies mainly in their combination of double suction water intake and centrifugal operation. Together with optimized hydraulic and structural design, this configuration increases flow capacity while maintaining stable operation and long service life.
Whether you are selecting a pump for a new project or managing an existing pumping system, understanding the working principle of a split case pump can help you choose the right equipment, reduce unnecessary costs, and improve overall system efficiency.
Founded in 2010, Purity has obtained more than 130 patent certifications and has an annual pump production capacity of over 150,000 units. Its products are exported to more than 140 countries and regions worldwide. Over the years, Purity Pump has continuously invested in product research and development and manufacturing process improvements, providing stable and reliable pump products and professional system solutions for different applications.
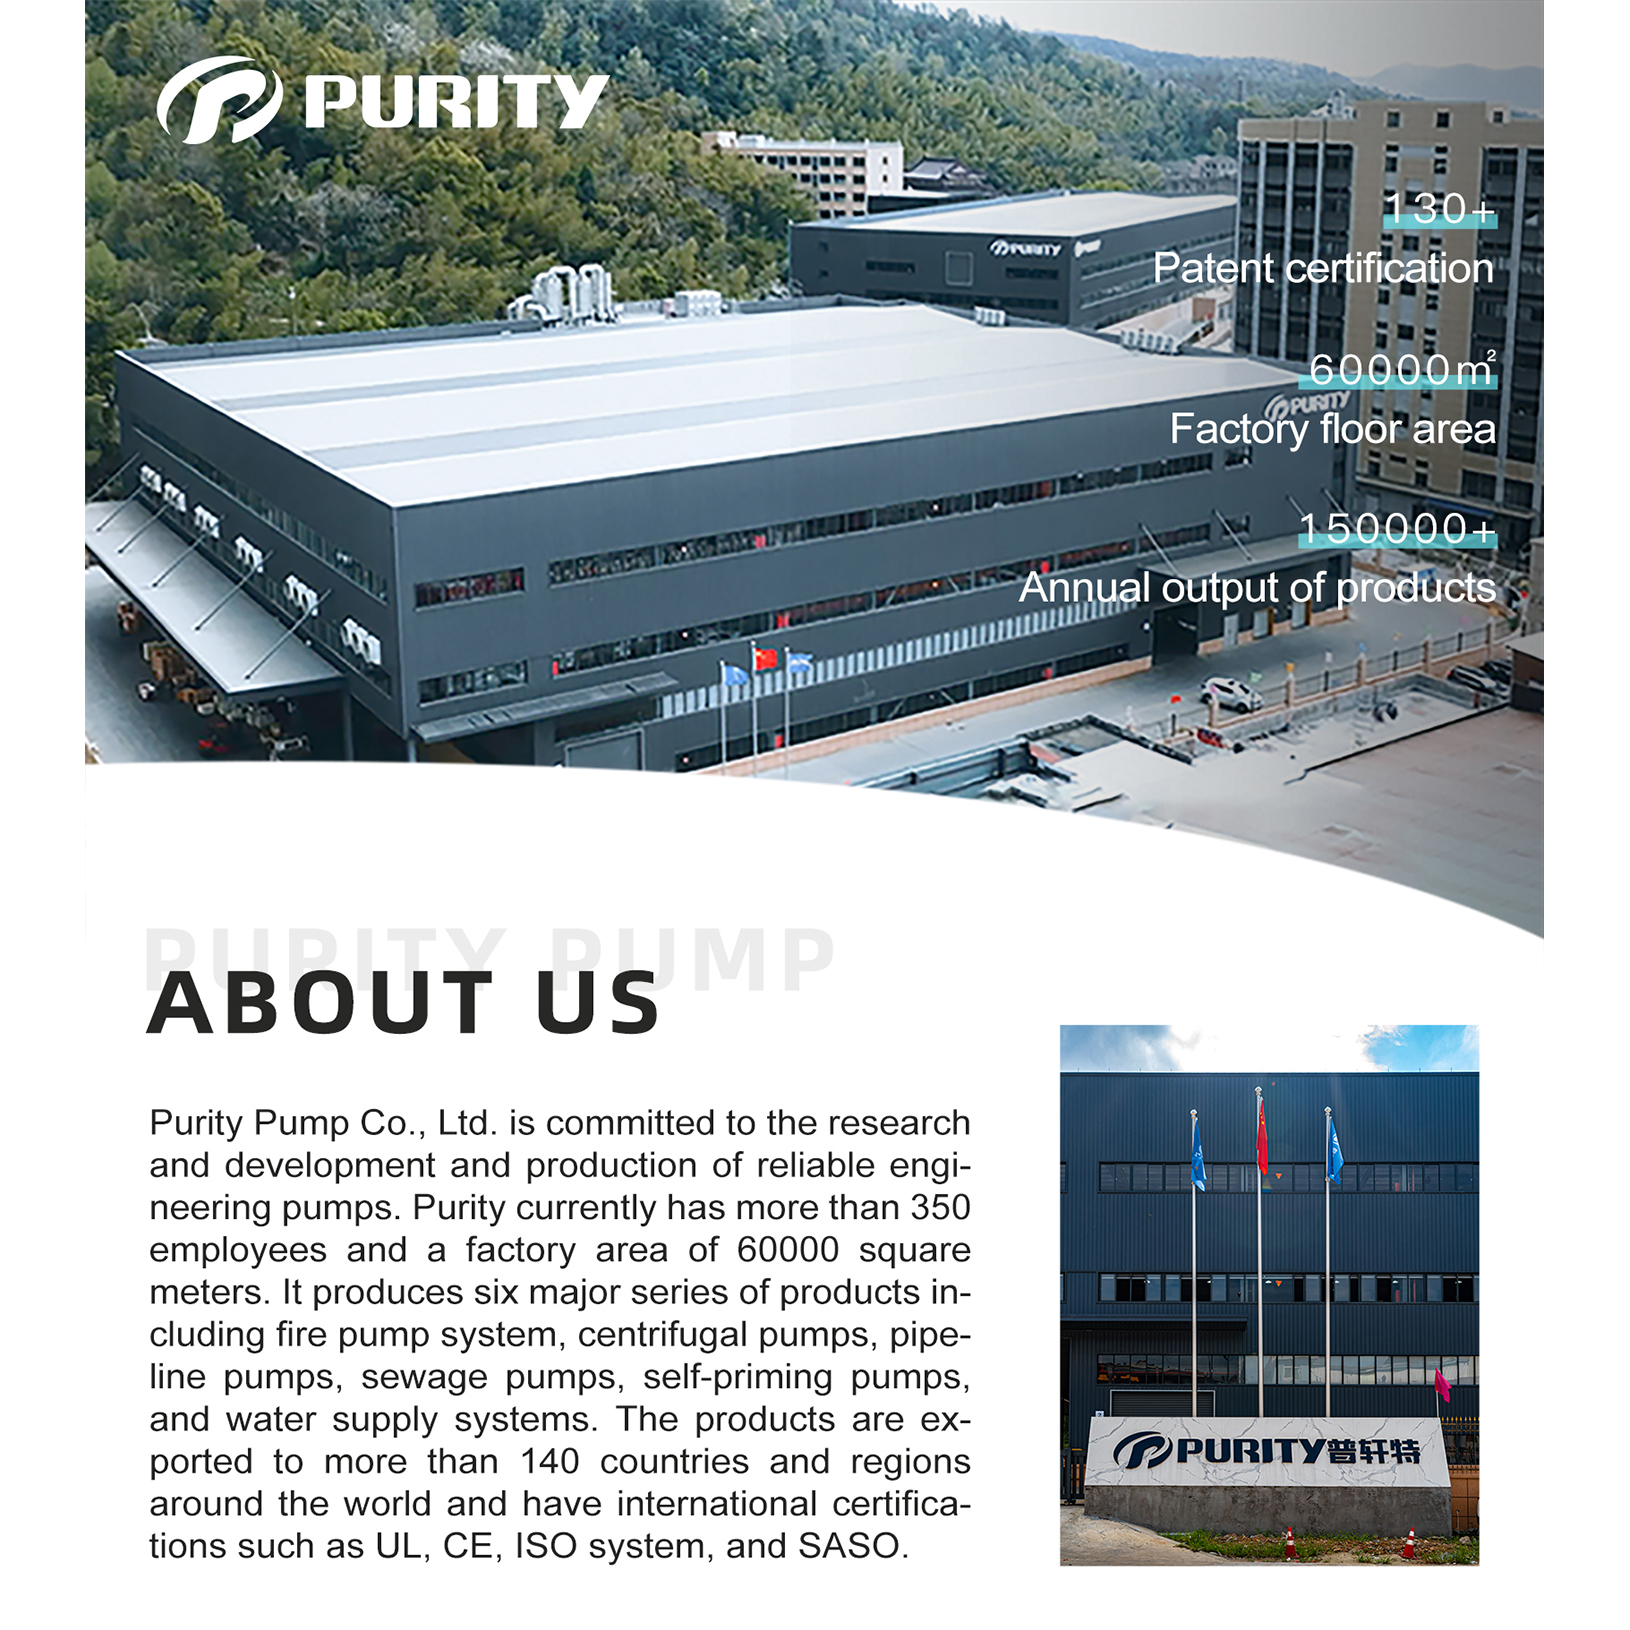
Picture|Detailed Information About Purity Company
If you are looking for a split case pump for water supply, circulation, agricultural irrigation, or other high flow applications, feel free to contact Purity. We can provide detailed product specifications, application recommendations, and distributor support based on your actual operating conditions.
Post time: Oct-09-2026